Moisture Balance
Explore a range of moisture balances and moisture analyzers designed for the rapid determination of moisture content in laboratory samples and materials.
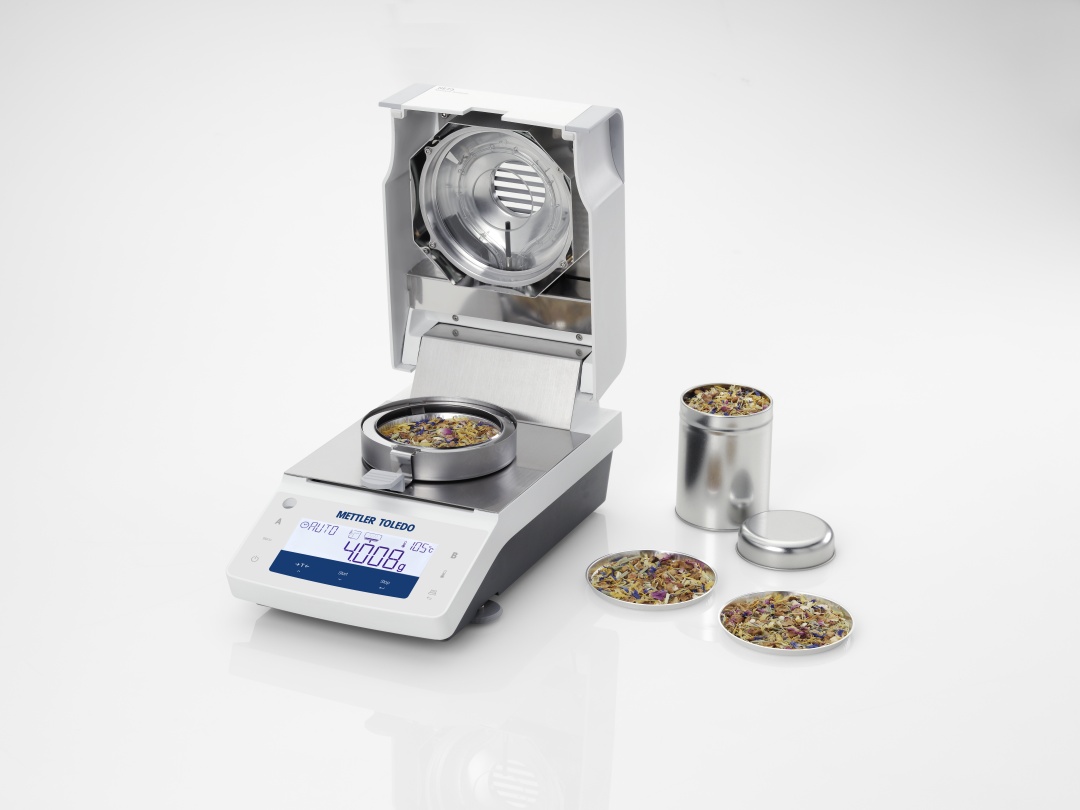
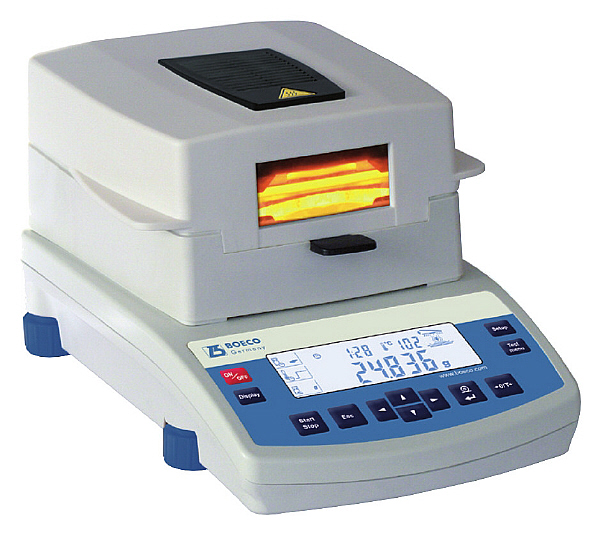
Moisture balances combine weighing and controlled heating to determine the moisture content of a sample. The instrument continuously monitors the sample's weight during the drying process and calculates the moisture loss, providing a convenient method for moisture analysis compared with conventional drying and weighing procedures.
Moisture analyzers are commonly used for moisture content testing, quality control, raw material inspection, product development, production monitoring and laboratory analysis. They can be applied to a wide variety of materials, including food products, chemicals, pharmaceuticals, powders, granules and other suitable samples.
Depending on the model, features may include digital weighing systems, halogen or infrared heating, programmable temperature settings, drying profiles, automatic endpoint detection, moisture percentage display, residual moisture measurement and data connectivity.
Suitable for food and beverage laboratories, pharmaceutical facilities, chemical laboratories, research and development, manufacturing, agricultural testing, educational institutions and industrial quality control laboratories, moisture balances provide a practical solution for rapid moisture determination.
When selecting a moisture balance, consider the weighing capacity, readability, moisture measurement range, heating method, temperature range, drying time, sample type, endpoint detection and data recording requirements.